Abrasive powders can shorten the stable operating window of a jet mill when nozzle condition is left outside the test and maintenance plan. The useful question is not how long a nozzle will last in the abstract. It is what wear-sensitive parts, material conditions, particle-size acceptance limits and inspection records must be defined before production starts.
Quick Answer
- Nozzle wear should be treated as a process-control and maintenance question, not only a spare-parts question.
- Abrasiveness, feed size, moisture, target particle-size distribution, gas condition, operating time and contact-material choices can all affect the inspection plan.
- Do not promise a nozzle life from a material name alone. Establish a baseline on representative material, record the tested conditions, and define the trigger for engineering review.
- For an abrasive-powder project, ask the supplier to define the nozzle and wear-part scope alongside the mill, classifier, collection and test-report scope.
Why Nozzle Wear Belongs in the Production Plan
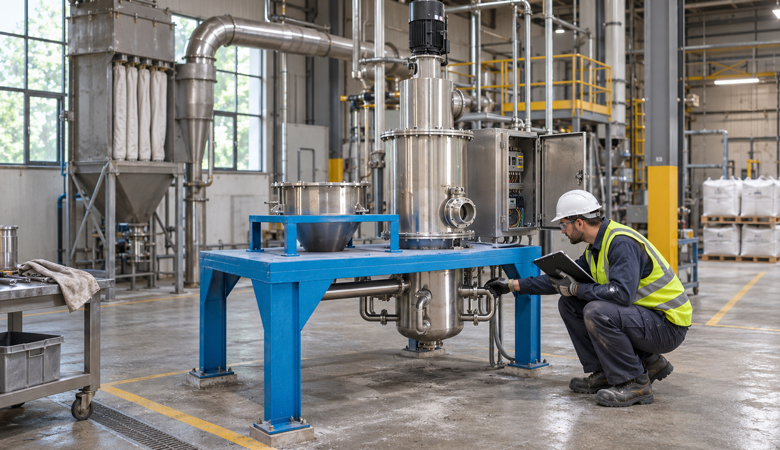
A jet mill uses dried compressed air or another approved process gas to accelerate powder through nozzles. Particle-to-particle impact performs much of the size reduction, while the internal classification stage separates accepted fine powder from material that needs more grinding. For abrasive material, the gas path and powder-contact surfaces deserve early review because wear can change the operating condition that produced the original test result.
The Mills Powder Jet Mill product page describes the core system as nozzles, a grinding chamber, built-in classification and cyclone/bag-filter collection. That system boundary matters: a nozzle discussion that ignores feeding, classification and collection cannot establish whether a later PSD change is a wear issue or a wider process change.
What Wear Can Change and What It Cannot Prove
Wear is not proof that a product is out of specification, and a changed PSD is not proof that nozzles are the cause. Feed condition, classifier setting, air supply, sampling method and collection behavior can also change a test. The right response is a controlled comparison against an agreed baseline rather than a claim based on appearance alone.
| Review item | Why it matters | Record before production |
|---|---|---|
| Representative material | Hardness, particle shape and contaminants can change the wear question. | Material identity, current feed PSD, moisture, bulk density and safety notes. |
| Wear-sensitive scope | Nozzle, liner and classifier contact surfaces may need different review. | Specified contact materials, drawing/revision reference and included spare-parts boundary. |
| Operating basis | A result is only comparable when its test conditions are known. | Gas type/condition, pressure basis, feed method, classifier setting and run duration. |
| Product acceptance | A single average size may miss an oversize risk. | Target D50/D90/D97 or top cut, allowed oversize and measurement method. |
| Inspection decision | A visual check alone cannot define process impact. | Who checks, what is measured, review trigger and disposition path. |
Start With a Representative Abrasion Review
Material name alone is not enough. Two powders sold under the same family name may differ in feed-size range, mineral impurities, particle shape, moisture, agglomeration or required fineness. Those differences can affect feeding stability, impact conditions and the part of the system most likely to need attention. Send a representative sample and the current particle-size report where available; do not extrapolate a short trial into an unconditional production-life statement.
For hard ceramic materials, the existing ceramic powder jet mill selection guide already explains why contact materials, nozzle wear, classifier wear, collection and cleaning must be evaluated together. This article has a narrower job: it sets out how to turn that concern into an inspection and comparison plan after the process route is chosen.
Define the Baseline Before You Need It
The most useful baseline is a dated, reproducible record of a representative run. It should identify the material and feed condition, gas supply condition, feed method, classifier setting, collection boundary, sampling point and PSD method. Record qualified-product output separately from feed rate; they are not interchangeable. If the process uses a target top cut, state the instrument and reporting basis instead of writing only a micron number.
The goal is not to impose one universal inspection interval. It is to make future comparisons possible. An engineering review is warranted when a measured process result, inspection observation or operating change departs from the agreed baseline and ordinary operating adjustments do not explain it. The supplier and buyer should agree who authorizes a change to nozzles, liners, classifier components or acceptance conditions.
A Practical Inspection and Comparison Sequence
- Confirm the lot, feed-size condition, moisture status and target PSD before the run.
- Record the approved gas and operating basis, including the measurement basis for pressure or flow used by the project.
- Use the agreed sampling point and PSD method; retain the raw report or a traceable summary.
- Inspect agreed accessible wear-sensitive components during planned downtime, following the project safety and isolation procedure.
- Compare the finding with the baseline record. Escalate to engineering when the inspection or process result no longer supports the agreed operating and acceptance basis.
- Document the disposition: continue with monitoring, revise a condition, replace a defined part, or schedule a controlled retest.
When a Jet Mill May Need Another Route or More Testing
A jet mill is not automatically the first choice for every abrasive powder. Very high throughput, limited compressed-air infrastructure, wet or strongly agglomerated feed, a relatively coarse target, or an application that cannot tolerate the uncertainty remaining after a representative test may point to a different process route or pre-treatment step. The question should be decided with material, PSD, capacity and site data, not by a generic wear claim.
Buyers considering the wider machine configuration can also review Fluidized Bed Opposed Jet Mill What Buyers Should Confirm Before Quotation. Its focus is system selection and quotation scope; use this wear-plan article to add an operating baseline and maintenance-review question to that earlier decision.
Questions to Put in the RFQ and Test Plan
| Question | Why ask it |
|---|---|
| Which components are in the wear-sensitive scope for this material and target PSD? | Clarifies the engineering boundary without assuming every part has the same exposure. |
| What material and operating conditions will the sample test document? | Makes the result useful for a production comparison. |
| How are feed rate and qualified-product output distinguished? | Avoids a capacity number that cannot be compared later. |
| What PSD method and acceptance limits apply? | Connects inspection decisions to a measurable product requirement. |
| What inspection access, spares and change-control responsibilities are included? | Prevents maintenance scope from becoming an unrecorded quotation gap. |
FAQ
Does every abrasive powder require the same jet mill nozzle material?
No. Material behavior, contamination limits, target PSD, run conditions and the supplier design must be reviewed together. A material name is not enough to select a contact material or promise service life.
Can nozzle wear be judged from a particle-size result alone?
No. A PSD shift can have several causes. Compare representative material, gas condition, feed method, classifier setting, sampling method and inspection observations with a documented baseline.
What information should I send before a wear review?
Send material identity, current feed PSD and moisture, target D50/D90/D97 or top cut, required feed and qualified-product rate, contamination limits, available gas data, application and any prior test report.
Can a lab trial guarantee production maintenance intervals?
No. A lab or pilot trial helps define direction and a baseline, but it does not establish an unconditional production interval. Production configuration and operating conditions require their own documented review.
Engineering Summary
For abrasive-powder jet milling, plan nozzle and wear-part review as part of the process specification. Use representative material, a defined operating basis, a PSD method and a written inspection decision path. This approach does not promise wear life; it gives the buyer and supplier a way to detect and discuss a change before it becomes an untraceable production problem.
Conclusion
If you are planning an abrasive-powder jet mill project, contact Mills Powder with the material data, target PSD, capacity basis, gas and site conditions, contamination limit, and any existing test records. The review can then define whether testing, contact-material options, inspection access or a different process route needs further engineering work.